:sales@zsjhsteel.com WhatsApp:+86-15122582058


ZSJH


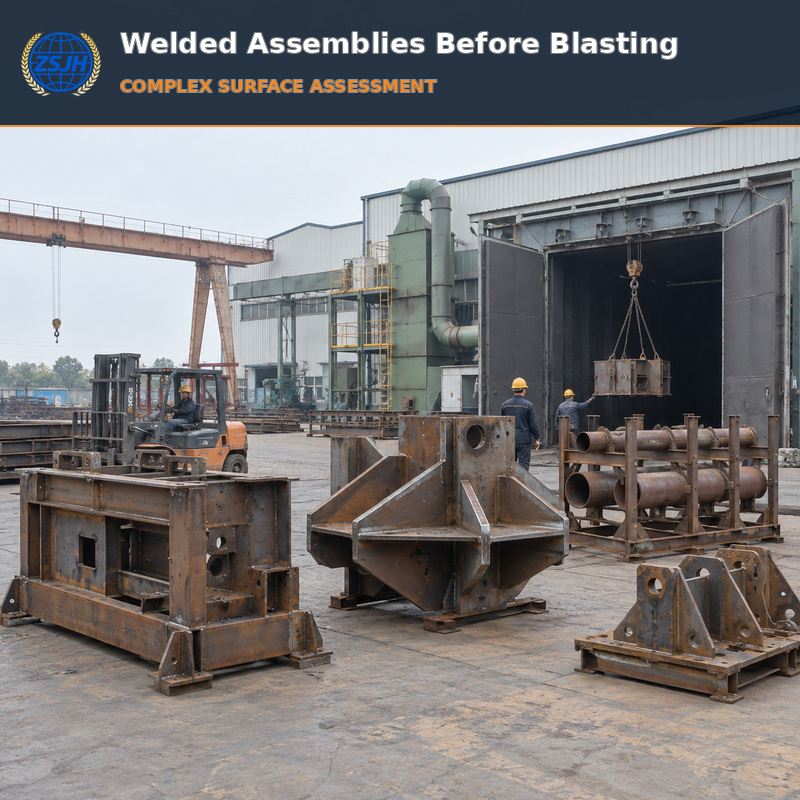
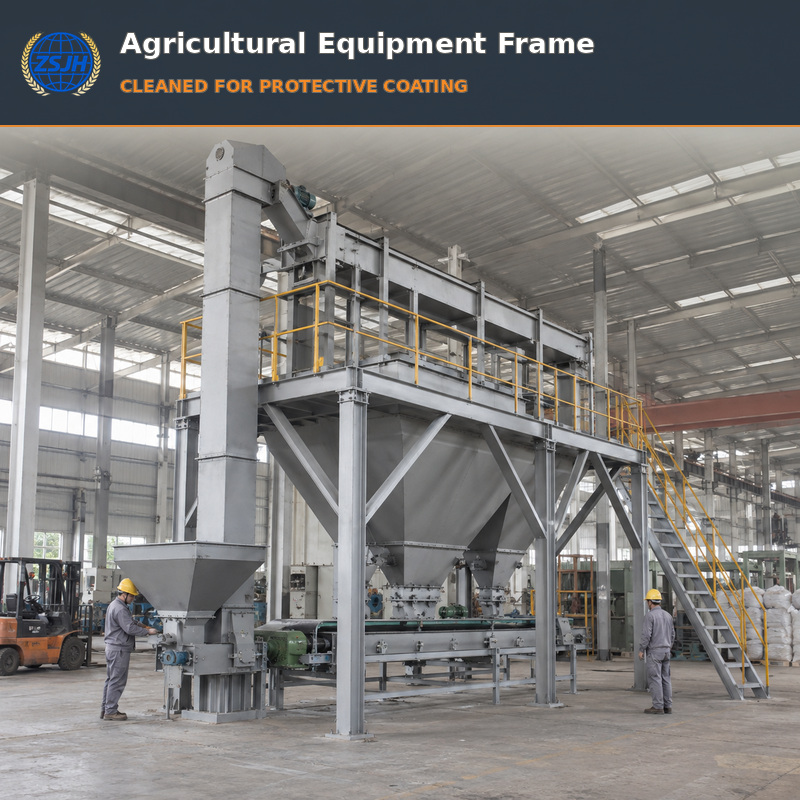
ZSJH evaluates the steel condition, component geometry, welded details, protected interfaces, handling requirements and next coating process before blasting. Abrasive selection, machine route, pass count and local manual treatment are coordinated with the approved specification. Final acceptance can include visual cleanliness, surface profile, dust condition and other agreed checks. Cleanliness designations such as Sa 2, Sa 2.5 or Sa 3 are used only when required by the approved project standard. Prepared s is protected from recontamination and flash rust, then transferred to the next process within the agreed time window.
Differentiation Factor | Service Requirement |
Service scope | Abrasive shot or blast cleaning before coating |
Applicable steel | welded frames, brackets, nodes, stiffened components and assembled steel parts |
Cleaning target | specified visual cleanliness with supplementary local preparation where direct blasting is limited |
Profile requirement | According to coating data sheet and approved specification |
Inspection | Visual condition, profile and agreed contamination checks |
Output | Cleaned steel released for the approved next treatment |
· Initial surface condition assessed before processing
· Cleaning route matched to component geometry and size
· Specified cleanliness and surface profile controlled separately
· Edges, welds and restricted areas receive planned treatment
· Post-blast protection and transfer timing are controlled
· Weld discoloration
· Spatter
· Scale
· Fabrication rust and contaminants in corners
Cleaning grade, abrasive type, target profile, component orientation, protected and masked areas, local touch-up, dust acceptance, inspection points, post-blast holding time and subsequent treatment can be customized for welded steel assembly shot blasting according to the approved coating system and equipment capacity.
· Review initial condition, drawings and next coating process
· Confirm component size, weight and handling route
· Protect machined surfaces, threads and specified interfaces
· Complete controlled blasting and local follow-up treatment
· Remove dust and inspect cleanliness and surface profile
· Record agreed inspection results
· Protect and transfer steel promptly to the next treatment
· Incoming surface-condition record
· Surface-cleanliness inspection report
· Surface-profile measurement report when specified
· Dust or additional contamination test record when required
· Nonconformance and local rework record
· Release record for the next coating process
Send your component drawings, initial surface photos, dimensions, target cleanliness and coating requirements to ZSJH for a review of the welded steel assembly shot blasting and a detailed quotation.


